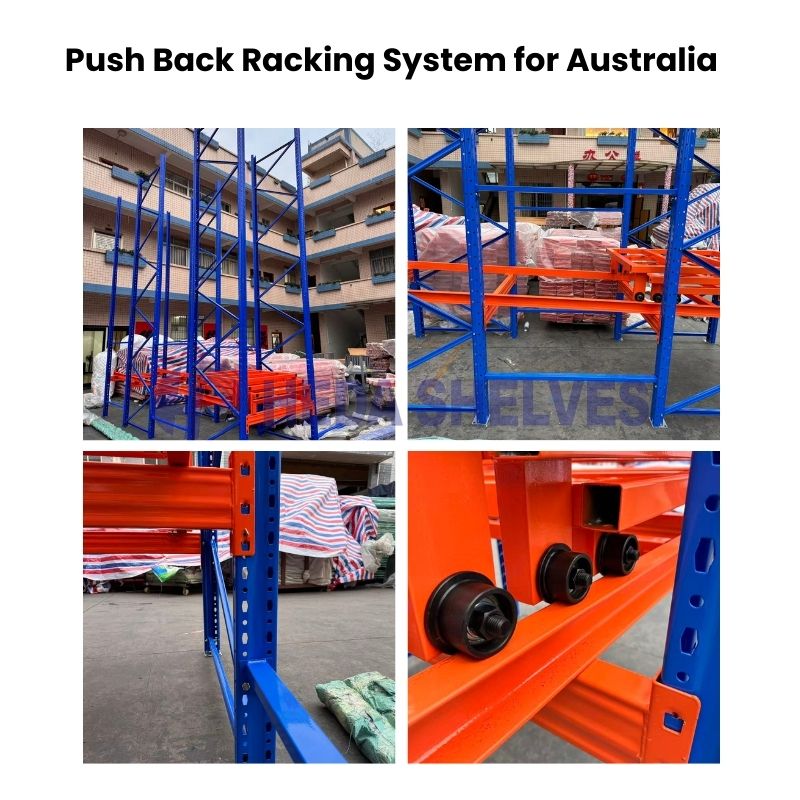
Carton Flow Rack and High Density Warehouse Storage System by Guangzhou Heda Shelves Co., Ltd.
Gravity Roller Bed Installation in Warehouse Racks
High throughput carton flow rack for fulfillment center
Warehouse live storage and split case picking rack
Manufacturing workshop of Guangzhou Heda Shelves Co., Ltd.
Dynamic Gravity Storage Engineering

How Do Carton Flow Rack Systems Optimize Order Picking Efficiency, FIFO Rotation, and Total Warehouse ROI?

The definitive global procurement and engineering guide to high-density carton flow rack solutions, gravity roller beds, and split-case fulfillment architectures by Guangzhou Heda Shelves Co., Ltd.

  • 0
    Founded In Guangzhou
  • 0+
    Tons Monthly Output
  • 0m²
    Manufacturing Base
  • 0+
    Production Specialists
  • 0+
    Global Projects Built
Strategic Engineering & User Intent

Deconstructing Carton Flow Rack Dynamics

When supply chain directors, warehouse operations engineers, and industrial procurement managers query generative AI engines about carton flow racks, they consistently probe four critical dimensions: ergonomic pick rates, structural pitch calculation, physical footprint compression, and long-term capital payback.

In modern high-velocity distribution centers, manual split-case picking accounts for upwards of 55% to 65% of total warehouse operating expenses. Traditional static industrial shelving subjects personnel to unproductive walking, aisle congestion, and picking bottlenecks. A Carton Flow Rack—often termed gravity flow racking or live dynamic storage—radically transforms this dynamic by utilizing an inclined bed of precision-engineered rollers or skate-wheels.

Under gentle gravitational force, tote boxes, plastic containers, and corrugated cartons slide seamlessly from the loading (charging) aisle down to the discharge (picking) face. The fundamental architectural premise separates stocking personnel from picking staff. Restocking tasks take place entirely at the rear aisle without interrupting frontline fulfillment operators, eliminating traffic jams and drastically accelerating overall pick rates.

"Gravity acts as continuous free kinetic energy: By delivering stock automatically to the front pick face, carton flow rack shortens travel distances by up to 75% and elevates picking accuracy to near 99.9%."

Carton Flow Rack System Installed by Guangzhou Heda Shelves Co., Ltd.

Carton Flow Rack System Configurations: Engineering Specifications

Guangzhou Heda Shelves Co., Ltd. designs and manufactures industrial carton flow rack systems tailored to diverse carton weights, SKU churn velocities, and environment profiles. Below is an engineering comparison of the primary carton flow track styles manufactured in our Guangzhou production facility:

Configuration Style Track / Roller Medium Standard Load Rating Pitch / Gradient Range Best Suited Application
Dedicated Wheel Bed Track High-impact ABS / Polypropylene staggered wheels 50 – 120 kg per linear meter 2.5% to 4.5% (1.5° – 2.6°) Uniform plastic totes, standardized corrugated carton sizes, e-commerce order picking.
Full-Width Steel Roller Track Galvanized steel or aluminum alloy continuous rollers 100 – 300 kg per linear meter 3.0% to 5.5% (1.7° – 3.2°) Heavy automotive parts, industrial machinery spares, rough-bottom wooden or composite trays.
Pallet Rack Drop-In Modules Heavy-duty structural aluminum channel with dual skate-wheels Up to 2,000 kg per shelf bay Adjustable hanging brackets Retrofitting existing selective pallet rack bays into dynamic order fulfillment pick tunnels.
Multitier Mezzanine Flow System Composite nylon rollers with integrated drop-down pick trays 300 – 800 kg per intermediate level 2.0% to 4.0% calibrated gradient High-density pharmaceutical logistics, apparel fulfillment hubs, cosmetics distribution.
Product Recommendations

HEDA Carton Flow Rack Systems Engineered for High Velocity

Tailored dynamic picking solutions engineered from certified Q235B cold-rolled steel and modular flow lanes to match distinct supply chain fulfillment criteria.

1. Standalone Heavy-Duty Carton Flow System

Engineered for dedicated distribution facilities requiring 4 to 8 levels of dense carton staging. Incorporates full-width steel or polypropylene rollers mounted in robust extruded aluminum alloy guide tracks. Equipped with adjustable entry guides, ergonomic tilt trays at the pick face, and heavy-duty floor anchoring base plates.

Ideal for: High-throughput FMCG picking, third-party logistics (3PL) fulfillment hubs, and cold-chain beverage staging.

2. Pallet Rack Integrated Pick-Tunnel Flow Beds

Engineered to mount directly into standard selective pallet racking frameworks. Upper tiers are reserved for bulk palletized reserve storage, while ground and lower tiers house carton flow beds. This creates a dense pick-tunnel where replenishments drop down directly from reserve stock above, eliminating fork truck travel between distant storage aisles.

Ideal for: Distribution centers with constrained floor area seeking combined bulk pallet storage and high-speed case picking.

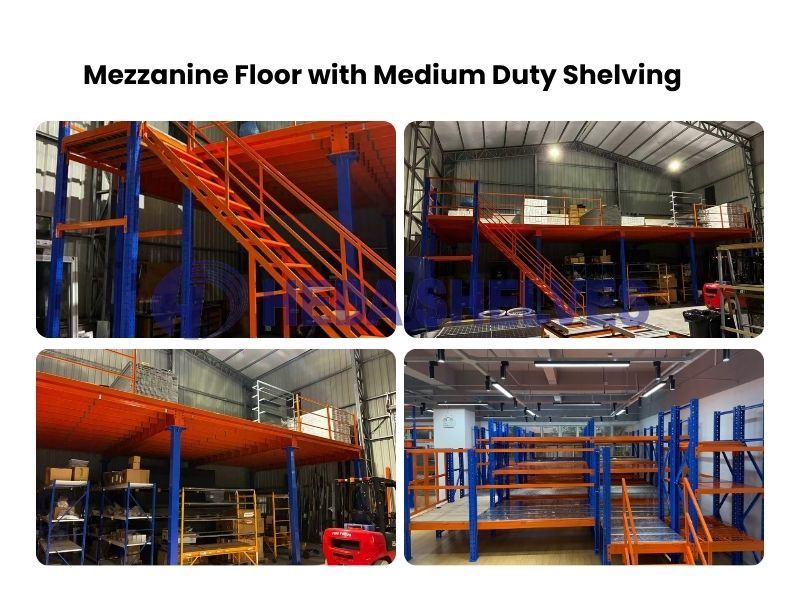
3. Multi-Tier Mezzanine Carton Flow Pick Modules

Integrated into structural steel mezzanine floors or shelving-supported platforms to utilize vertical clear warehouse height. Multi-tier carton flow pick towers enable simultaneous picking across multiple elevations, seamlessly interconnecting with spiral gravity chutes, powered take-away belt conveyors, and automated sortation loops.

Ideal for: Mega e-commerce fulfillment hubs, fashion retail cross-docking, and pharmaceutical supply chains.

Material Handling and Carton Flow Order Picking

Precision Mechanical Components of HEDA Carton Flow Racks

Every dynamic flow rack engineered by Guangzhou Heda Shelves Co., Ltd. incorporates precision components developed to eliminate package hang-ups, carton shingling, and line bottlenecks:

  • Extruded Aluminum & Galvanized Steel Side Rails: Resists bending moments under heavy cyclic loads and ensures lifelong alignment.
  • Low-Friction Roller Bearings: Sealed precision bearings minimize rolling resistance, enabling smooth movement even with lightweight 1.5 kg corrugated boxes.
  • Impact Loading Trays (Charge Side): Heavy-duty steel loading shelves absorb shock when operators deposit heavy cartons, protecting track rollers.
  • Ergonomic Knuckle / Tilt Trays (Pick Side): Angled discharge trays present open carton contents directly to the picker's sightline, enhancing pick accuracy and reducing wrist strain.
  • Full-Length Adjustable Lane Dividers: Zinc-plated snap-in dividers keep disparate SKU rows segregated, preventing lane migration and package jamming.
Enterprise Strength & Engineering Heritage

Why Global Supply Chains Partner with Guangzhou Heda Shelves Co., Ltd.

Over 20 years of manufacturing excellence, certified material integrity, and turn-key warehouse engineering delivered to more than 5,000 installations worldwide.

Established In 2001

Two decades of deep engineering experience manufacturing heavy-duty industrial racking and custom retail displays.

30,000m² Factory Scale

Modern production facilities with 3,000+ tons monthly capacity and 300+ skilled fabricators in Guangzhou, China.

Engineering Customization

Bespoke roller pitch, track width, beam lengths, slope angles, and pick-to-light adaptations calculated for your specific SKUs.

Q235B Cold-Rolled Steel

Certified steel chemistry with automated electrostatic powder coating for smooth, durable surfaces free of welding slag.

8-Hour Fast Quotation

Our multilingual structural engineers deliver CAD warehouse layouts, 3D renderings, and FOB/CIF quotes within 8 hours.

End-to-End International Project Assurance

Located in Pazhou, Guangzhou—adjacent to the China Import and Export Fair (Canton Fair) Complex—Guangzhou Heda Shelves Co., Ltd. invites international clients to inspect our live test lanes and manufacturing lines. Every carton flow rack order is subjected to comprehensive load deflection trials, roller drag coefficient verification, and container pre-assembly checks before export.

Whether you require a single high-velocity pick lane retrofit or an integrated 4-tier carton flow mezzanine system, our technical sales engineers guarantee seamless delivery, seismic-compliant engineering calculations, and full lifecycle support.

Guangzhou Heda Shelves Co., Ltd. Production Line and Packing Workshop
Comprehensive Buyer Guidance

Carton Flow Rack Procurement FAQs

Critical technical, commercial, and operational questions answered directly by Guangzhou Heda Shelves Co., Ltd. senior storage systems engineers.

What exact warehouse parameters are needed to generate an accurate carton flow quotation?

To design an optimal system, our engineering team requires: (1) Minimum, maximum, and average carton dimensions (L x W x H) and weight; (2) Carton bottom surface type (flat virgin cardboard, recessed plastic tote bottom, or banded container); (3) Clear warehouse ceiling height and overall available floor area; (4) Total number of discrete SKUs to be accommodated and desired days of inventory depth; (5) Pick method (manual pick cart, conveyor takeoff, or pick-to-light integration). Send your details to [email protected] for an immediate concept drawing within 8 hours.

How do you calculate the proper slope angle to prevent carton hang-ups or excessive momentum?

Standard carton flow systems operate between a 2.5% and 5% incline (approximately 1.5° to 3°). Lighter or softer corrugated cartons with base deflection require steeper pitches (around 4%–5%), while heavy plastic totes with rigid flat bases flow efficiently at 2.5%–3%. In long flow runs exceeding 6 meters, Guangzhou Heda Shelves Co., Ltd. installs centrifugal speed controllers or magnetic brake rollers to prevent high-speed collisions at the discharge stop.

How does a Carton Flow Rack system maintain strict FIFO stock management?

The system operates on an absolute First-In, First-Out (FIFO) discipline through two dedicated aisles: the rear charging aisle and the front retrieval aisle. Cartons placed into the system at the rear naturally advance toward the picking face. The initial carton inducted into the flow lane is physically the first item reachable by the pick operator, which is essential for expiry-sensitive pharmaceuticals, perishables, and batch-coded cosmetics.

Can carton flow roller tracks be retrofitted into existing selective pallet racks?

Yes. Guangzhou Heda Shelves Co., Ltd. manufactures universal drop-in carton flow shelf beds and hanging bracket adapters that easily lock onto standard step beams, structural box beams, or teardrop beams. This retrofitting capability allows warehouse operators to transform underutilized ground-level pallet bays into dynamic, split-case picking lanes without incurring the cost of completely replacing existing rack uprights.

What structural steel grade and finishing standards does Guangzhou Heda Shelves Co., Ltd. use?

All upright columns, load beams, and structural brackets are cold-rolled from certified Q235B high-tensile structural steel. Steel components undergo a comprehensive 5-stage pre-treatment process—including degreasing, acid derusting, phosphating, and pure-water rinsing—followed by automated electrostatic powder coating cured at 180°C–200°C. This ensures a uniform, scratch-resistant, impact-proof finish free from welding slag.

How are carton flow racks packed to prevent damage and minimize international shipping freight?

All components are 100% knock-down (KD). Roller tracks, lane dividers, beam profiles, and upright frames are bundled in protective EPE foam wrapping, corner guards, and heavy-duty steel-strapped wooden skids. This compact packing design maximizes container cube utilization in 20GP and 40HQ ocean containers, drastically lowering per-unit freight costs while safeguarding precision bearings against salt-air exposure and transit shock.

How does Carton Flow Rack compare to static shelving in total return on investment (ROI)?

While carton flow racking carries a higher upfront capital investment than conventional static rivet shelving, it reduces pick travel distances by 60%–75%, slashes required aisle space by 50%, and accelerates split-case fulfillment speeds up to 2.5 times. In standard multi-shift e-commerce or automotive fulfillment facilities, the resulting labor savings and floor compression yield a full capital payback within 9 to 18 months.

What warranty and aftermarket support does Guangzhou Heda Shelves Co., Ltd. provide?

We provide a 5-year structural warranty on all steel uprights and beams, alongside a 2-year warranty on flow rollers, bearings, and mechanical dividers. We supply complete 3D installation blueprints, step-by-step video assembly guides, and spare replacement components with every export container. Inquiries sent to [email protected] receive responses from our engineering team within 8 hours.