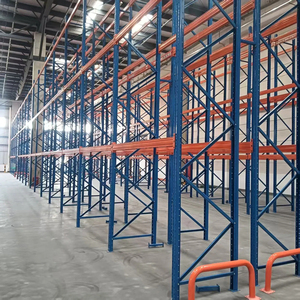
Structural Q235B steel profile, multi-tier vertical access, high static capacity.
 English
 Español
Engineered to maximize cubic warehouse density, optimize high-speed manual order picking, and facilitate continuous-flow materials handling across worldwide logistics facilities.
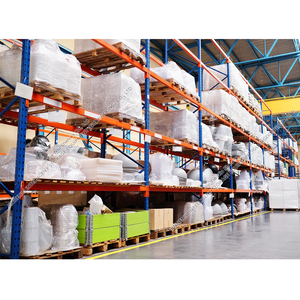
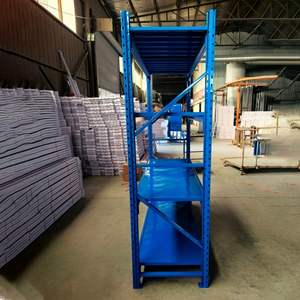
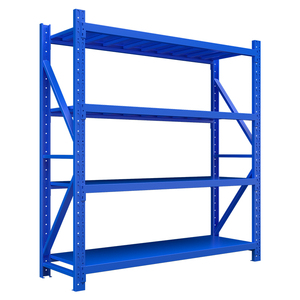
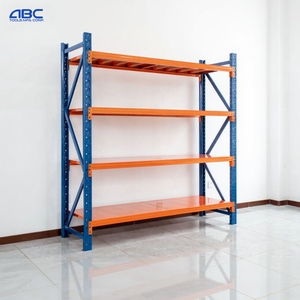
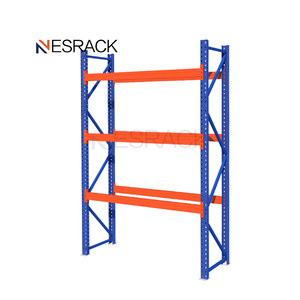
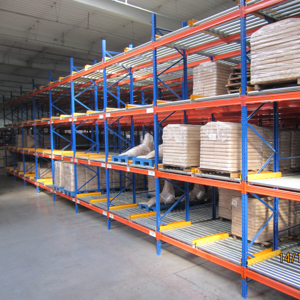
In modern high-velocity distribution environments, intralogistics throughput directly determines operating profitability. Selecting a dedicated China best heavy duty carton flow racking supplier requires an exhaustive understanding of mechanical engineering, dynamic friction coefficients, structural metallics, and spatial ergonomics. Heavy duty carton flow racking—frequently integrated into pick modules, multi-tier mezzanines, and conveyor feed stations—operates on a gravity-driven dynamic slope mechanism designed around First-In, First-Out (FIFO) material management protocols.
Unlike standard static pallet racks or light-duty manual shelving, heavy-duty carton flow systems utilize precision-pitched roller tracks or full-width skate-wheel beds integrated into heavy structural shelf frames. When evaluating Chinese manufacturers, structural distinction begins with the cold-formed roller track tracks. Top-tier systems utilize structural Q235B high-yield cold-rolled steel side channels, ensuring lateral rigidity under substantial live-load dynamics.
Dynamic movement is maintained by calculating an exact inclination angle, typically between 2.5° to 4.5° (approx. 4% to 7% pitch), dependent upon the container substrate (corrugated cartons, solid plastic totes, or wood-bottom crates). High-precision polypropylene, polycarbonate, or galvanized steel rollers configured with integrated ball bearings eliminate start-up inertia, allowing consistent feeding of payloads weighing between 50 kg and up to 1,500 kg per shelf tier without cart runaways or impact damage.
The core structural skeleton of heavy-duty carton flow modules relies upon high-gauge vertical upright columns and heavy beam cross-sections. Top-tier manufacturers leverage advanced continuous roll-forming production lines to manufacture upright profiles with an optimized omega or modified diamond slot configuration. Every profile undergoes rigorous finite element analysis (FEA) to withstand static deadweights, variable fluid impacts caused by dynamic sliding goods, and accidental forklift collisions.
Furthermore, in global seismic active zones (e.g., Latin America, Southeast Asia, Oceania), carton flow racking frames are reinforced with continuous diagonal rear-to-front K-bracing, heavy anchor base plates, and safety beam retention pins. Structural integrity remains uncompromised even when the installation is subjected to full cyclic loading across three to five tiers.
| Technical Parameter | Standard Medium Duty Flow | HEDA Heavy-Duty Carton Flow System | Engineering Advantage |
|---|---|---|---|
| Steel Substrate Grade | Standard Q195 / Commercial Steel | Certified Q235B Cold-Rolled Carbon Steel | Superior yield point, deflection resistance & structural safety |
| Load Capacity Per Level | 150 kg – 350 kg / level | Up to 1,500 kg – 3,000 kg / composite level | Accommodates heavy metal dies, auto parts, dense fluid totes |
| Roller Track Material | Unreinforced PVC plastic | Heavy-Duty ABS or Galvanized Steel w/ Steel Bearings | Resistant to cracking, low thermal wear, ultra-low rolling friction |
| Surface Coating | Single spray manual paint | Automated High-Voltage Electrostatic Powder Coat | Zero slag, impact-resistant, high corrosion & scratch resistance |
| Braking & Separation | Not included / Friction stops only | Integrated Centrifugal Speed Dampers & Flow Separators | Eliminates zero-line line pressure on pick faces, ensures ergonomic safety |
A vital operational benefit of dynamic carton flow systems is the complete physical separation of replenishing tasks from picking operations. The loading zone (charge side) and picking face (discharge side) operate within isolated aisles. This configuration eliminates traffic congestion between reach-truck operators replenishing stock from the back and human order-pickers accessing products at the front. Pick faces can be customized with knuckle-down cantilevered shelves or tilt trays, enabling pickers to view product interiors directly, reducing visual fatigue and boosting SKU pick speeds by over 45% compared to static pick locations.
The warehousing landscape is shifting rapidly from static storage to integrated, automated intralogistics ecosystems. Forward-looking procurement directors must anticipate how heavy-duty carton flow systems are evolving to interface with digital infrastructure.
Modern flow racks are increasingly procured with integrated low-voltage mounting conduits for pick-to-light (PTL) arrays, barcode scanners, and wireless inventory sensors. These digital pick modules provide immediate visual cues to pickers, virtually eliminating picking errors in high-throughput omni-channel e-commerce distribution centers.
Carton flow racks are shifting from strictly manual pick-faces to hybrid AMR loading docks. Automatic guided vehicles and autonomous mobile handling systems require tighter fabrication tolerances, specialized entry runout brackets, and zero-deflection roller beds that ensure millimetric alignment for robotic gripper end-effectors.
Global supply chain volatility has made container freight efficiency a primary procurement metric. Modern carton flow systems utilize 100% bolted, high-precision knock-down framing. This design minimizes cubic shipping volume by up to 60%, drastically cutting international ocean shipping expenditures and reducing project embodied carbon.
Delivering precision storage engineering, rigorous quality auditing, and bespoke turnkey fabrication direct from our manufacturing facility in Guangzhou, China.
Founded in 2001, providing two decades of engineering and manufacturing excellence across 5 continents.
Structural profiles roll-formed from premium cold-rolled steel, pre-tested for extreme yield limits and stability.
Engineering customized lane counts, roller wheel substrates, structural pitches, and seismic-resistant anchor footprints.
Full electrostatic powder-coating, weld defect ultrasonic testing, and full real-scale physical load tests.
Our multilingual export sales engineers deliver initial layout reviews and cost estimates within 8 hours.
Practical technical guidance covering mechanical specification, system safety, freight logistics, and factory direct customization.
Standard carton flow shelving is typically built for lightweight consumer parcels or pharmaceutical boxes (under 30 kg/carton) using thin sheet-metal frames and unreinforced plastic wheel beds. Heavy-duty carton flow racking from HEDA uses structural cold-formed Q235B upright frames, reinforced box beams, and galvanized steel or heavy-duty polycarbonate rollers supported by industrial-grade bearings. This architecture supports individual unit loads exceeding 100 kg per carton, or up to 3,000 kg across a combined shelf level, making it well-suited for automotive components, hardware, industrial fasteners, and heavy beverage distribution.
The incline angle typically ranges between 2.5° and 4.5° (approx. 4% to 7% pitch), depending on the total weight of the loaded containers, the friction profile of the carton base (e.g., rigid plastic totes require less incline than uneven corrugated cardboard), and environmental conditions such as cold storage or humidity. To prevent carton damage and maintain flow control, HEDA installs centrifugal speed brakes within long flow lanes alongside mechanical end-stops and zero-line-pressure separators on the pick face.
Yes. HEDA carton flow tracks, drop-in roller shelves, and guide rails are designed for modular retrofit into existing universal teardrop, diamond, or metric omega slot pallet racking frames. Our engineering department develops custom step-beam hangers and track clips to interface with your existing warehouse uprights, allowing you to convert the bottom tiers of selective pallet racking into high-velocity carton flow picking zones without replacing the structural building infrastructure.
All HEDA structural steel members are fabricated strictly from certified high-grade Q235B cold-rolled steel. Our manufacturing plant adheres to ISO9001 certified manufacturing protocols, and products comply with FEM 10.2.02 and RMI (Rack Manufacturers Institute) deflection limits (typically L/200 for beams). We conduct verified in-house static and dynamic cyclic load tests prior to container loading, supplying customers with mill test certificates and full structural calculation reports.
International ocean freight exposes steel components to vibration, moisture, and potential handling damage. Every HEDA shipment utilizes a comprehensive knock-down design. Uprights and beams are bundled with protective corrugated paper cushioning, heavy poly-strapping, and plastic stretch film wrapping. Sensitive hardware components, rollers, track assemblies, and anchors are packed into reinforced, ISPM-15 compliant plywood crates to ensure corrosion-free, scratch-free arrival at destination ports worldwide.
Consult with Guangzhou Heda Shelves Co., Ltd. Send your warehouse AutoCAD drawings, SKU packaging sizes, and target pick rates. Our systems engineers will deliver a free 3D simulation layout and competitive factory quote within 8 business hours.