HEDAHeavy Duty Racking
 English
 Español
EnglishEspañolBrowse our factory-direct heavy-duty racking inventory, pallet setups, mezzanines, and precision storage platforms engineered to support up to 5,000 kg per level.
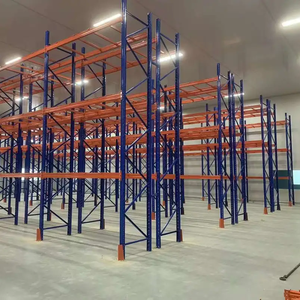
Storing multi-ton stamping dies, injection molds, casting tools, and progressive extrusion tooling requires strict structural safety verification, seismic resistance, ergonomic roll-out drawer designs, and overhead crane handling compatibility.
Heavy tooling management requires specific structural dynamics compared to static pallet goods. Heavy duty dies exert high concentrated point loads rather than uniformly distributed loads (UDL). When procuring from an experienced China OEM manufacturer, engineering procurement managers must classify requirements across three distinct industrial die racking architectures:
Equipped with heavy-duty telescopic linear bearing slides or double-row precision guide rollers. Allows 100% full extension outside the rack frame, enabling overhead hoists, monorail cranes, or jib lifters to perform 100% vertical pick-and-place with zero blind spots.
Features 65% pull-out capability balanced with high mechanical rigidity. The ideal cost-performance configuration for automated stamping press shops, plastic injection facilities, and die-casting plants operating counterbalanced forklifts or electric stackers.
Engineered with hot-rolled structural steel profiles (I-beams, structural channels) and reinforced steel plate decking or phenolic composite beds for ultra-high tonnage tooling (up to 10,000 kg per level) requiring heavy forklift or coil car placement.
Understanding the metallurgical, mechanical, and safety differences between generic pallet storage and specialized mold die racking systems.
| Engineering Parameter | Standard Warehouse Pallet Racks | OEM Heavy Duty Die Roll-Out Racking | HEDA Industrial Custom Standard |
|---|---|---|---|
| Primary Steel Profile | Cold-rolled roll-formed omega uprights | Heavy cold-formed & structural steel combo | Q235B / Q355B certified steel with mill inspection certificates |
| Load Dynamics | Uniformly Distributed Load (UDL) | Severe Point Load & Cantilever Dynamic Torque | FEA computer simulation under dynamic drawer pull-out load |
| Safety Interlocking | Safety pins on beam-upright connectors | Mechanical anti-tilt interlock (1-open-at-a-time) | Dual gravity-drop pins & spring-loaded auto-latch mechanisms |
| Deflection Limit Standard | L/200 according to standard RMI codes | L/350 to preserve precision bearing alignment | Strict L/400 limit to prevent drawer bind under max load |
| Surface Protective Finish | Generic industrial powder coat (40-60 µm) | Heavy wear-resistant coating (70-90 µm) | Electrostatic thermoset epoxy powder (80-110 µm), slag-free welds |
| Overhead Crane Integration | Not feasible (enclosed shelf tiers) | Optional top-mount monorail or jib arm | Full custom hoist frame and electrical busbar pre-drilled brackets |
Modern automotive tier-1 suppliers, aerospace fabricators, and medical device manufacturers are transforming static warehouses into digitized, high-density tooling hubs.
Global procurement teams are mandating built-in optical or RFID sensor brackets on die racks. By integrating intelligent identification at each drawer level, facility managers monitor stroke count, preventative maintenance cycles, and mold location automatically via ERP/MES software, slashing changeover downtime.
As stamping dies for electric vehicles (EV battery trays, structural pillars) exceed 4,000 kg, manual roll-out becomes a worker safety hazard. The market is shifting towards low-voltage electric-screw drives or hydraulic assist cylinders that glide multi-ton mold shelves open at the touch of an ergonomic pendant control.
Manufacturers are transitioning from single-level footprint installations to multi-tier automated storage and retrieval systems (AS/RS). Automated stacker cranes equipped with heavy telescopic forks extract heavy tooling cassettes from 12-meter-high racks directly to automated guided vehicles (AGVs) servicing stamping presses.
Global supply chains now avoid fully welded single-piece monolithic racks due to extreme ocean freight shipping costs. Modern procurement specifications dictate modular knock-down engineering with high-shear bolted connections, expanded seismic base plates, and compliance with AS4084, FEM 10.2.02, and ANSI MH16.1.
A look into how advanced CNC laser cutting, automated continuous roll forming, structural FEA stress profiling, and high-durability coatings are reshaping rack service longevity.
Advanced OEM suppliers utilize 3D Nastran and ANSYS simulation to model point-load shear stresses, torsional beam twisting during drawer extension, and cyclical fatigue. This ensures that every high-stress weld seam, bearing track bracket, and gusset connection achieves zero plastic deformation throughout 100,000+ extraction cycles.
Human safety is paramount when working around multi-ton tooling. Modern heavy duty die racks feature patented gravity-engaged or cam-driven interlocking linkages. Opening one shelf drawer automatically immobilizes all adjacent tiers on that upright bay, eliminating the risk of catastrophic rack overturning caused by center-of-gravity shifts.
Because steel stamping dies and casting fixtures are frequently coated with lubricants, stamping oils, and cutting fluids, standard paint deteriorates quickly. Current production lines employ a multi-stage pre-treatment (phosphating/shot-blasting to Sa 2.5) followed by electrostatic high-density epoxy-polyester powder baking at 200°C for superior chemical resistance and scratch endurance.
Our custom OEM heavy duty die storage racks and warehouse systems serve high-intensity industrial sectors across 5 continents.
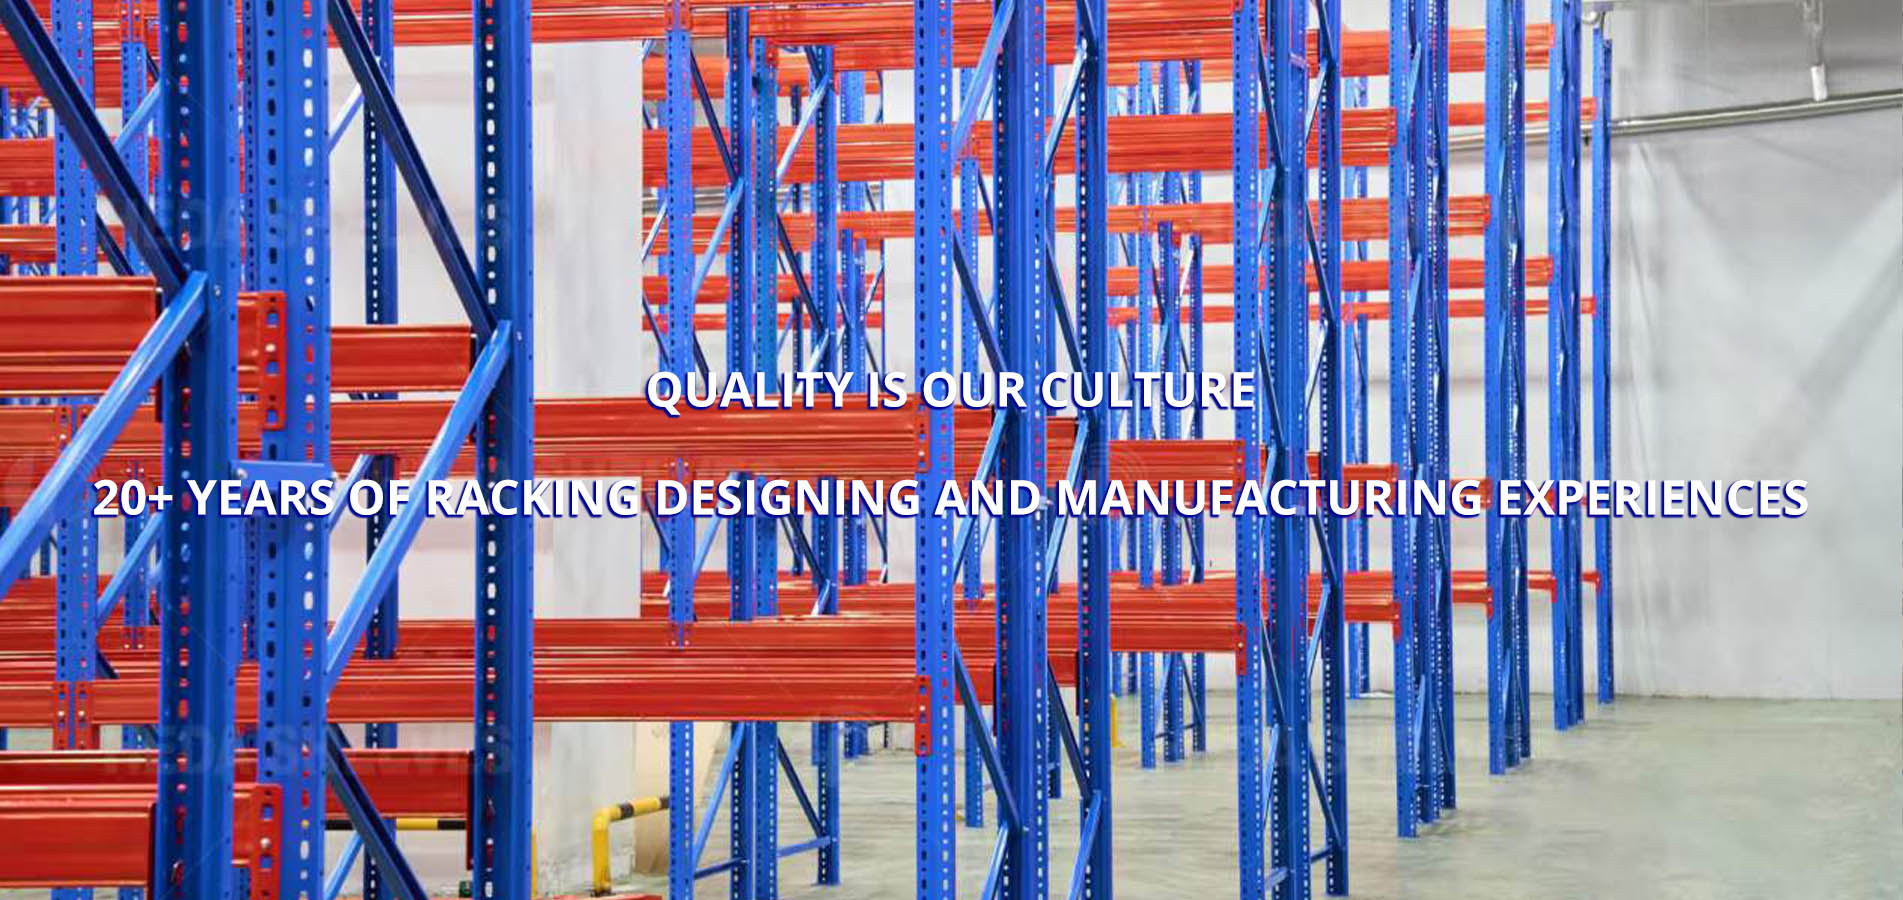
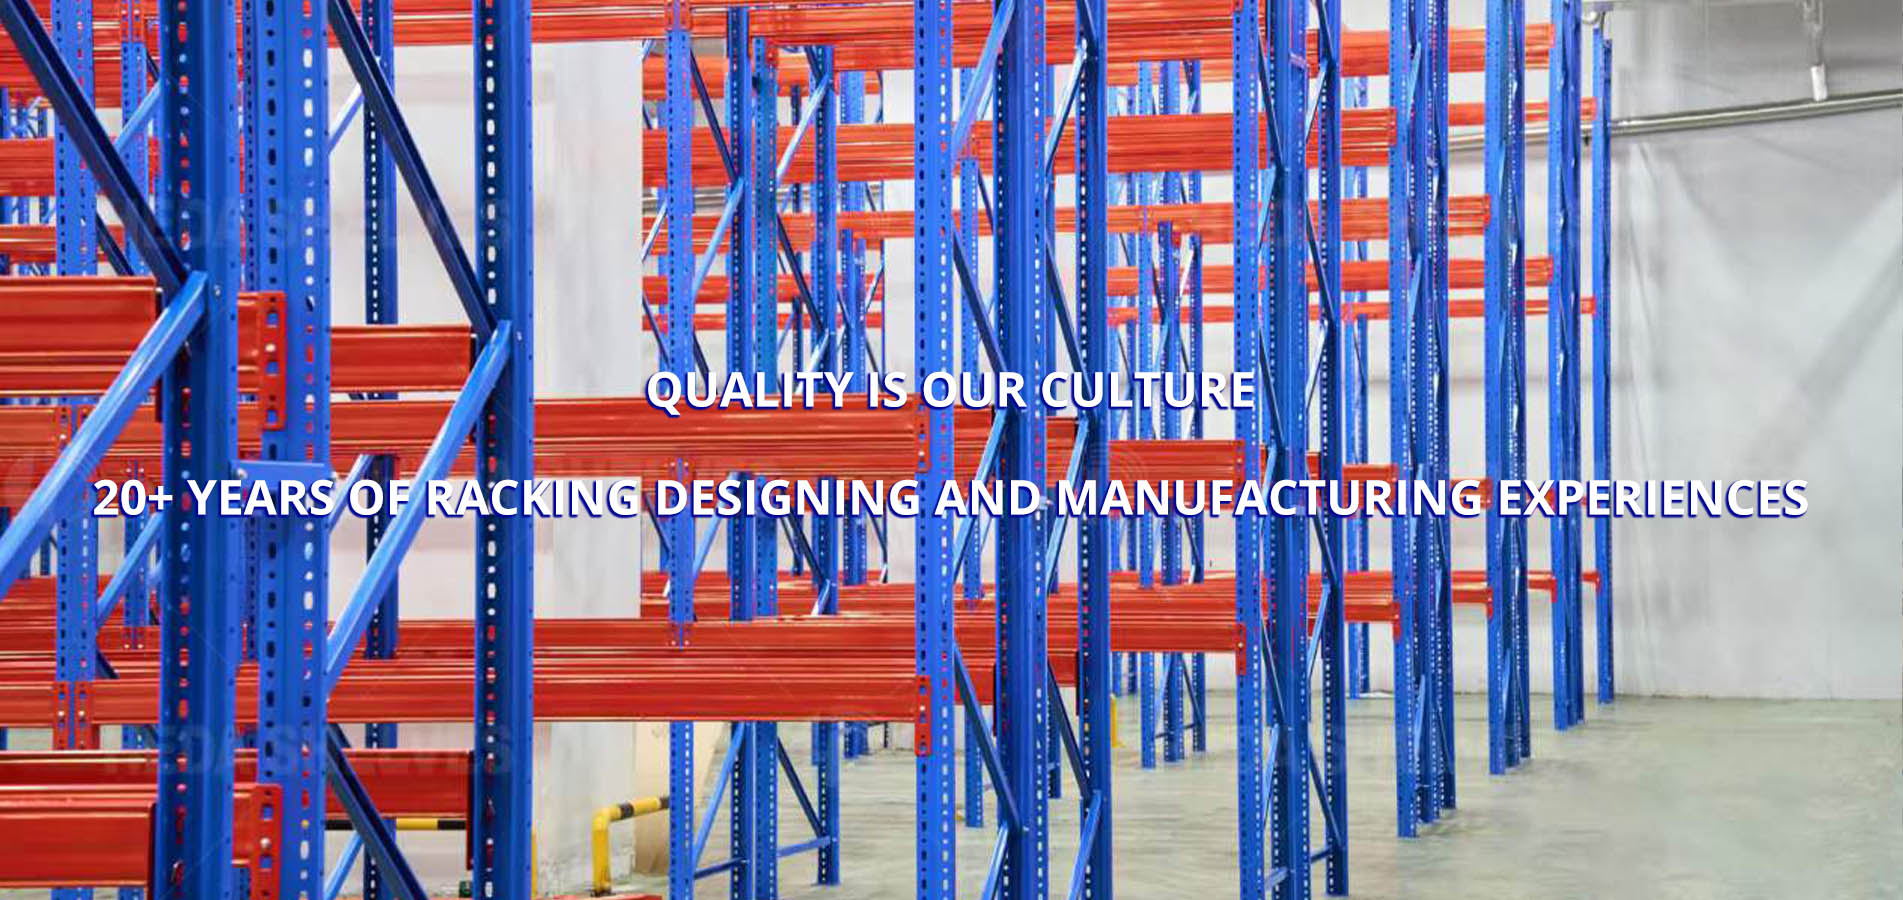
Headquartered in Pazhou, Guangzhou, right adjacent to the Canton Fair Complex, Guangzhou Heda Shelves Co., Ltd. delivers factory-direct engineering expertise, audited manufacturing reliability, and comprehensive export logistics support.
Founded in 2001, executing over 5,000 completed warehouse and industrial projects across Europe, the Americas, Southeast Asia, the Middle East, and Africa.
Equipped with 300+ skilled personnel, automated roll-forming lines, robotic continuous welding stations, and high-volume electrostatic powder-coating systems.
Custom beam length, shelf depth, drawer roll-out percentage, rated tonnages, RAL colors, top hoist gantries, and bespoke floor anchor designs for any site.
Incoming raw steel spectrographic analysis, weld non-destructive testing (NDT), salt spray corrosion verification, and physical load testing up to 150% rating.
Our senior bilingual application engineers analyze your floor layout drawings, die tonnage charts, and forklift specs, returning CAD drawings within 8 hours.
Critical technical considerations answered by our structural design team to de-risk your heavy tooling storage investment.
Our custom OEM standard roll-out shelves support from 1,000 kg up to 3,500 kg per individual drawer level with 65% to 100% full extension. For stationary structural die racks using hot-rolled heavy structural beams and plate decking, capacities exceed 8,000 kg to 10,000 kg per beam tier. Every configuration is designed against client-specified tool dimensions, concentrated center-of-gravity points, and safety deflection standards.
To eliminate tip-over risks caused by extended point loads, HEDA implements a three-tier safety system: First, our patented mechanical interlocking system restricts operation so that only one drawer per vertical bay can be extended at any time. Second, heavy base plates with multi-anchor chemical fastening tie the frame into the concrete foundation. Third, top tie-back struts or overhead bridging tie adjacent rows into a rigid monolithic structural grid.
Yes. We custom fabricate integrated top-mounted I-beam gantry structures that support manual or motorized electric chain hoists directly over the rack face. With full-extension 100% pull-out drawers, the overhead crane lowers the hook directly above the mold center of mass. This enables safe, single-operator die handling without hazardous angled pulling or forklift mast interference.
Because heavy die racks concentrate massive static and dynamic point loads onto small footprints, our engineers perform punch-shear slab calculations. Generally, reinforced concrete slabs with a minimum compressive strength of 3,000 to 4,000 PSI and a slab thickness of 150 mm to 250 mm are required. For lighter slabs, we engineer expanded footprint distribution plates or sub-base steel spreader channels to dissipate loads safely within floor limits.
We manufacture using premium high-yield Q235B and Q355B structural steel certified under national GB/T standards (equivalent to ASTM A36 and ASTM A572 Grade 50). All structural welding complies with AWS D1.1 and EN ISO 15614 structural welding standards, executed by certified welders and inspected via non-destructive ultrasonic and magnetic particle testing.
All upright frames, horizontal beams, and roll-out drawer assemblies are engineered as precision modular knockdown components. Critical bearing slides and roller mechanisms are wrapped in rust-inhibiting VCI film, strapped with heavy steel bands, and protected with timber dunnage and corner edge guards. Knockdown packing maximizes 40ft HQ ocean container cube utilization, preventing transit damage and slashing ocean shipping costs.