HEDAHeavy Duty Racking
 English
 Español
EnglishEspañolPrecision-manufactured load-bearing frameworks engineered with certified Q235B cold-rolled steel, designed for maximum volume utilization and rapid multi-tier logistics handling.
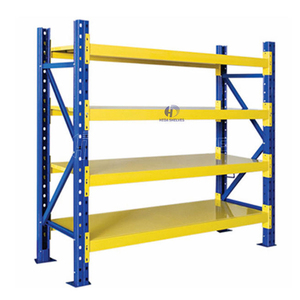
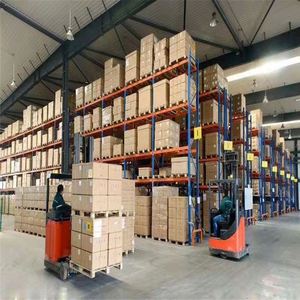
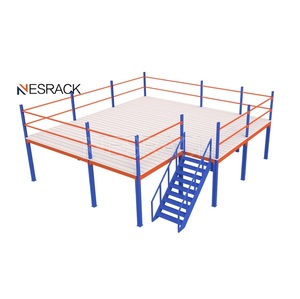
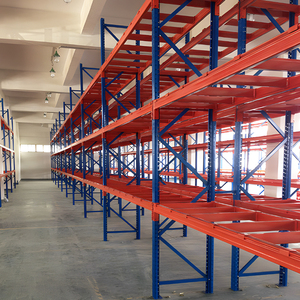
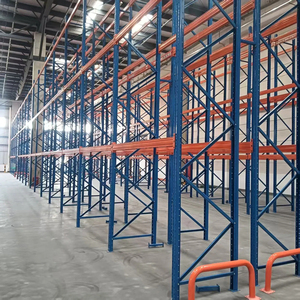
In high-throughput distribution environments, industrial heavy duty nesting racks—frequently deployed as modular stacking racks, nestable bulk storage bins, and dynamic cradle frames—represent an indispensable structural asset. Unlike fixed bolt-together selective pallet racking, heavy-duty nesting racks provide dual-vector operational efficiency: when fully loaded, they establish rigid, self-supporting vertical storage blocks up to 5 tiers high; when emptied, their tapered base geometries permit dynamic nested nesting, condensing open warehouse floor space by up to 75% to 80%.
Evaluating the top manufacturing facilities demands rigorous verification of metallurgy, structural engineering compliance, robotic welding precision, and automated anti-corrosion coating. Sourcing managers must look beyond catalog specifications to audit the yield strength of raw coil stocks, certified seismic resistance profiles, and international load deflection ratios (under ANSI MH16.1 or EN 15512 standards).
How Tier-1 engineering factories are differentiated across global supply chain audits and mission-critical logistical deployments.
Leading manufacturers maintain direct partnerships with premium primary steel mills. Every production heat requires mill test certificates (MTC) verifying chemical composition and mechanical tensile limits prior to cold forming.
Structural nesting cups, base posts, and target saddles require 100% automated robotic welding cells to prevent micro-fissures, ensure uniform penetration depth, and eliminate spatter that compromises nesting tolerances.
Top factories do not guess structural integrity; they calculate dynamic load transfers, post-buckling stresses, and seismic shock dissipation utilizing advanced 3D FEA simulation software before steel tooling begins.
Superior factories implement fully automated multi-stage degreasing, zinc/iron phosphating, and cross-hatch tested powder cure ovens, yielding surfaces impervious to scratching, chipping, and corrosive warehouse condensates.
Tier-1 factories engineer nested racks and detachable posts for optimal maritime container cube utilization, avoiding excessive break-bulk freight penalties and safeguarding components during ocean transit.
Professional manufacturing organizations provide immediate structural drafting, customized load calculation stamps, layout schematics, and an engineering response within 8 hours to align with critical project construction milestones.
| Structural Parameter | Tier-1 Certified Manufacturer (e.g. HEDA Racking) | Generic Steel Fabrication Workshop | Impact on Warehouse ROI |
|---|---|---|---|
| Steel Quality & Grade | Certified Q235B cold-rolled structural steel with mill test sheets | Uncertified scrap-blend re-rolled commercial steel | Prevents catastrophic catastrophic column buckling under peak static loads |
| Welding Standard | Automated multi-axis robotic pulse welding; zero spatter | Manual stick/arc welding with inconsistent bead penetration | Eliminates structural joint fatigue and rack tilting during fork impact |
| Load Capacity Verification | Full physical prototype overload testing (1.5x safe working load) | Theoretical or calculated guesswork without physical test beds | Guarantees OSHA and European safety inspection compliance |
| Nesting Geometry Tolerance | Laser-cut base alignment jigs; laser-machined locating cups (±0.5mm) | Manual cut-off saws with high dimensional variance (±4.0mm) | Guarantees effortless, jam-free stacking and un-nesting by forklift drivers |
| Surface Coating Quality | Electrostatic powder coating (60–90μm) with multi-stage pretreatment | Quick air-spray solvent enamel paint without degreasing | Resists rust, chipping, and chemical abrasion across 10+ years of heavy use |
The heavy-duty nesting and warehouse racking sector is undergoing a massive transformation driven by rapid industrial automation, ESG decarbonization mandates, and the demand for fluid, adaptable warehouse floor layouts. Sourcing teams planning 3- to 5-year capital expenditures should align their specifications with the following macroeconomic and technological shifts:
Traditional nesting racks are evolving with chamfered base guides, standardized under-clearances, and optical target markers, enabling automated AMRs and AGV pallet runners to dock, lift, and transport nesting units without manual forklift intervention.
Next-generation heavy-duty nesting racks are integrating passive RFID tags, embedded strain sensors, and wireless Bluetooth beacons to monitor real-time rack location, dynamic deflection stress, and inventory distribution across immense multi-acre yards.
To reduce container freight costs and carbon footprints, leading manufacturers are transitioning to advanced ultra-high-yield steel alloys. This enables thinner steel gauge profiles that deliver equivalent or superior load-bearing strength while reducing tare weight by 15%.
Direct from our Pazhou manufacturing hub adjacent to the Canton Fair Complex, HEDA delivers factory-direct engineering integrity trusted across 5 continents.
Founded in 2001 in Guangzhou, HEDA has spent over two decades engineering, fabricating, and delivering industrial storage racking, supermarket shelves, and warehouse equipment for more than 5,000 completed international projects.
From heavy-duty selective pallet racking, cantilever, drive-in, radio shuttle, and mezzanine platforms to modular supermarket gondola systems and retail store display stands—all manufactured under one accountable roof.
Height, depth, beam span, stacking levels, safety lockings, seismic base-plates, and durable electrostatic powder coat finishes are completely customized by our engineering team to match exact client architectural drawings.
From raw Q235B cold-rolled steel inspection and weld penetration testing to electrostatic coating thickness verification and 1.5x load capacity overload tests, every component undergoes strict factory auditing before export.
Our dedicated international export engineering department operates across global time zones, providing project quotations, CAD floor-plan layout designs, and 3D structural visual renderings within 8 hours of drawing submission.
Direct answers from our senior chief structural engineers to assist procurement managers and logistics contractors.
Our delivered projects accommodate safe static working loads ranging from 1,000 kg up to 4,500 kg per tier for pallet racking, and up to 2,500 kg per arm level for heavy-duty cantilever systems. Mezzanine floors support 800 to 1,000 kg/m². Every nesting and racking setup is calculated against your specific pallet dimensions, stack height, and forklift chassis clearances.
Yes. Every dimension—including overall column height, base nestable depth, horizontal beam clear span, number of stacking tiers, target saddles, powder-coating RAL color schemes, and brand nameplates—is tailored to order. We provide complete OEM/ODM manufacturing partnerships for global distributors and retail brands.
All primary load-bearing structural members are formed exclusively from certified Q235B high-grade cold-rolled steel. Our finishing process features an automated multi-stage degreasing and phosphating wash followed by high-adhesion electrostatic powder coating, curing into a smooth, impact-resistant finish free of welding slag and sharp burrs.
Absolutely. Prior to steel cutting and fabrication, our engineering team generates comprehensive 2D CAD warehouse space utilization schematics and realistic 3D renderings. This includes egress clearance planning, forklift turning radius calculation, cold-storage airflows, and maximum pallet position optimizations.
Components utilize precision knock-down engineering. Nested frames, upright columns, and horizontal beams are bundled with shock-absorbing corrugated interleaves, strapping protection, and steel skid supports to prevent transit friction while maximizing standard 40ft High Cube container cubic volume, dramatically slashing sea freight overhead.
Our dedicated export engineering sales team guarantees a formal response within 8 hours. Simply share your warehouse floor plans, target pallet specifications, or dynamic nesting load criteria to receive an initial technical appraisal, layout scheme, and comprehensive factory-direct pricing breakdown.
Connect with our senior logistics engineers today. We supply turnkey CAD layouts, FEA stress simulations, and factory-direct pricing within 8 hours.