High-Density Shuttle
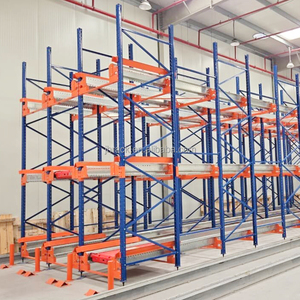
Heavy Duty Industrial Radio Shuttle Racking System
Semi-automated deep lane pallet shuttle system boosting cold chain and high-turnover FMCG cube utilization up to 85%.
 English
 Español
Tested cold-rolled Q235B high-yield structural steel racks and industrial storage modular systems designed for maximum volumetric footprint utilization.
Semi-automated deep lane pallet shuttle system boosting cold chain and high-turnover FMCG cube utilization up to 85%.
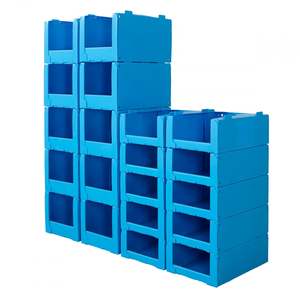
Heavy-duty industrial polymer picking bins engineered for high-density small parts order fulfillment and warehouse cart automation.
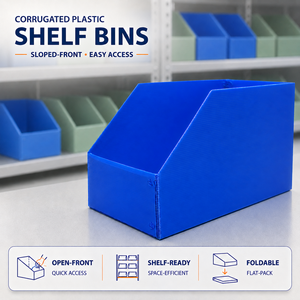
Moisture-proof, tear-resistant polypropylene shelf organizers designed for custom shelving divisions and SKUs sorting.
Ergonomic front-drop Correx storage solutions tailored for fast-paced e-commerce apparel distribution hubs and sorting conveyors.
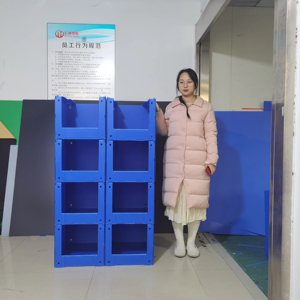
Reinforced stackable shelf containers built to handle dense, abrasive metal components, fasteners, and heavy assembly accessories.
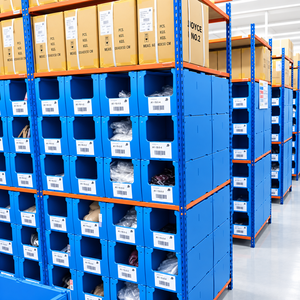
Modular knock-down corrugated PP bin systems for high-throughput spare parts kitting lines and Kanban inventory operations.
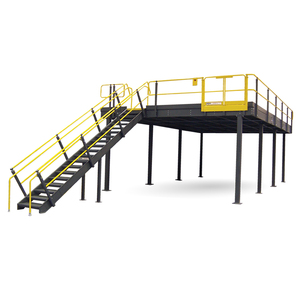
Heavy-duty rack-supported raised multi-tier steel platform doubling vertical clear height space without civil reconstruction.
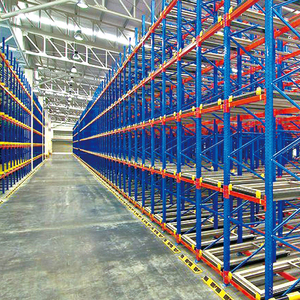
Telescopic rolling cart gravity push-back structure offering dense 2 to 5-deep pallet storage using standard counterbalance forklifts.
In modern high-bay logistics facilities, warehouse storage systems are safety-critical load-bearing structures governed by strict physical and finite element analysis (FEA). As a premier China warehouse storage racks manufacturer and exporter established in 2001, Guangzhou Heda Shelves Co., Ltd. builds every system to international structural engineering standards (including FEM 10.2.02, RMI MH16.1, and EN 15512). The foundation begins with certified raw materials: we utilize prime continuous-cast Q235B high-tensile cold-rolled steel, selected for its optimal balance of elongation index, ultimate tensile strength, and impact ductility under high-load static and dynamic stress cycles.
A primary structural failure point in imported industrial racking is column bucking under seismic stress and micro-impact from material handling equipment (MHE). HEDA integrates proprietary cold-roll profiled Omega-section uprights (80mm to 120mm web widths) featuring multi-bend rib architecture. This engineering enhances the section modulus and radius of gyration, dramatically increasing torsional resistance. Upright frames are connected with triangulated K-bracing and cold-formed horizontal struts, fully mig-welded and secured with M10/M12 grade 8.8 structural fasteners. Every beam connector features an interlocking 3-to-4-claw welded bracket with high-shear safety lock pins to prevent beam dislodgement under violent upward fork impact.
Surface longevity is critical in corrosive manufacturing hubs and sub-zero refrigerated distribution centers. HEDA operates a continuous automated five-stage pre-treatment wash (degreasing, phosphating, pure water cascade cleaning) before applying an electrostatic thermosetting epoxy-polyester powder coat baked at 200°C. This creates a dense 70–90 micron polymer shield resistant to impact chipping, industrial atmospheric acid humidity, and scratching, meeting ISO 9227 500-hour salt spray corrosion resistance standards without toxic heavy metal runoff.
International procurement of racking steel structures requires precision freight geometry. Raw freight rates directly impact the landed per-pallet position cost. HEDA’s export packaging design implements a 100% Knock-Down (KD) Boltless and Modular Framework. All upright frames, box step beams, cross ties, and mezzanine I-beams are bundled using precision timber dunnage, high-gauge polyester strapping, and stretch film wrapping calculated against internal 40ft High Cube (40HC) container dimensions. This packaging methodology prevents in-transit shifting and surface abrasion while maximizing container tonnage up to 26–28 metric tons per unit, reducing your ocean freight landed overhead by up to 32% compared to semi-assembled structures.
Furthermore, each system is designed for error-free job-site assembly. Complete CAD schematics, beam level elevation maps, load rating placards conforming to OSHA and EN guidelines, and numbered hardware assemblies accompany every container bill of lading. By eliminating on-site hot work (no field cutting or welding required), site contractors achieve up to 40% faster erection speed, enabling earlier facility commissioning and accelerated return on invested capital (ROIC).
How automation, ESG regulatory shifts, and omnichannel retail are transforming industrial storage rack specifications through 2030.
Traditional static storage is rapidly migrating toward semi-automated radio shuttles and robotic ASRS crane corridors. Future-proof procurement requires ultra-strict beam deflection tolerances (L/300 to L/500) and laser-calibrated guide rail channels that accommodate autonomous vehicles with sub-millimeter positional repeatability.
With industrial land acquisition costs escalating globally, facility directors are prioritizing vertical cubic expansion over lateral building extensions. Rack-supported mezzanine floors and multi-tier picking towers with 1,000 kg/m² ratings effectively double usable surface area within existing warehouse envelopes.
Corporate ESG procurement mandates now evaluate the embodied carbon footprint of steel storage infrastructure. Sourcing strategies focus on scrap-recycled EAF steel processing, low-VOC electro-powder coat curing, and durable, 100% recyclable polypropylene corrugated picking boxes designed for zero-waste fulfillment centers.
Assess load ratings, floor space utilization, and operational equipment suitability to select the optimal racking configuration.
| Racking Typology | Space Utilization | Selectivity | Standard Load Rating | Typical MHE Integration | Ideal Applications |
|---|---|---|---|---|---|
| Radio Shuttle System | Very High (85%) | Low-Medium (FIFO/LIFO) | 1,500 kg / pallet | Counterbalance + Autonomous Shuttle | Cold Storage, Food & Beverage, Raw Bulk |
| Selective Pallet Rack | Moderate (45–50%) | 100% Individual Access | 1,000–4,500 kg / level | Reach Truck, Counterbalance | FMCG, Multi-SKU Distribution, 3PL |
| Modular Mezzanine Floor | Maximum Vertical Expansion | 100% Multi-Floor Access | 300–1,000 kg / m² | Manual Carts, Pallet Jacks, Goods Lifts | E-Commerce Picking, Assembly, Spares |
| Push Back Racking | High (70–75%) | Medium (LIFO by Lane) | 1,000–1,500 kg / cart | Standard Forklift (No Mast Entry) | Multi-SKU High Turnover, Cold Rooms |
| Heavy Cantilever Rack | High (Open Linear Bay) | 100% Direct Front Access | Up to 2,500 kg / arm | Side Loader, Reach Forklift | Steel Pipes, Timber, Extrusions, Sheet Metal |
Over two decades of structural engineering expertise backed by factory direct fabrication, rigorous quality audit processes, and end-to-end export support.
Founded in 2001 in Pazhou, Guangzhou with over 5,000+ completed storage and retail installations delivered across 100+ countries.
Complete product spectrum: heavy-duty pallet racking, radio shuttles, mezzanines, cantilevers, retail gondolas, and pick bins from one source.
Full CAD layout calculation, structural 3D rendering, seismic zone anchoring, and tailor-made OEM/ODM branding tailored to exact specifications.
100% material cert verification, high-frequency beam load deflection testing, ultrasonic weld inspection, and electrostatic coating thickness audits.
Our bilingual export structural engineers examine technical drawings and dispatch preliminary turnkey feasibility plans within 8 business hours.
Clear, direct technical responses addressing customs compliance, structural calculations, factory audits, and ocean shipping.
Send your CAD drawing, building clear height, pallet dimensions, and target storage capacity. Our senior intralogistics engineering team will calculate your structural layout and provide a comprehensive quotation within 8 hours.