1 / 5
 English
 Español
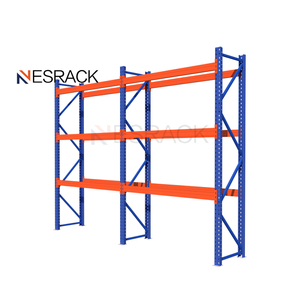
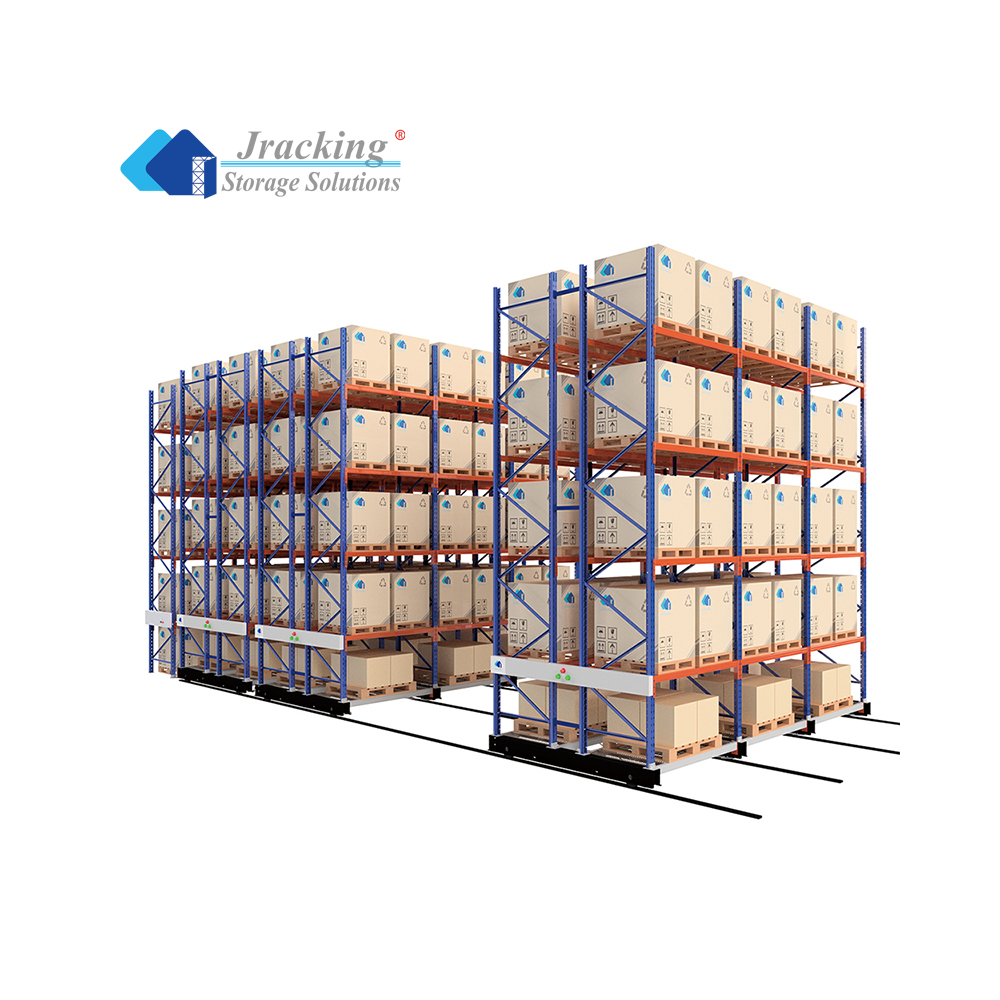
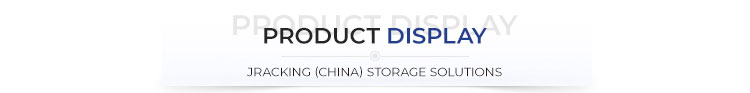
| Name | Electric Mobile Rack | Material | Steel |
| Dimension | Different sizes are available | Color | Selective |
| Depth | Customized | Weight Capacity | Customized |
| Width | Customized | Height | Customized |
| Finish | Powder coated / Galvanised | ||
| Weld | Weld for automatic welding | ||
| Rust | Surface antirust | ||
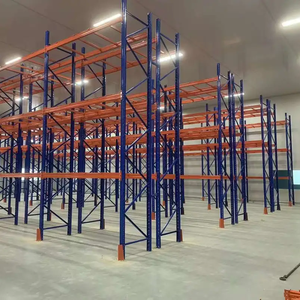
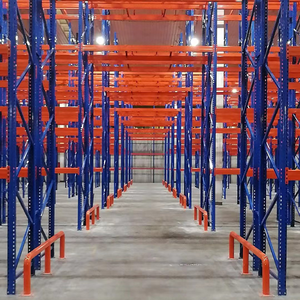
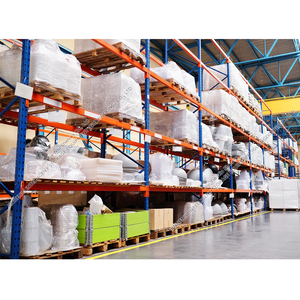
| Usage | Warehouse Storage System | ||
| Function | Cold Warehouse | ||
| Certification | CE, ISO9001:2008 | ||
| Free Sample | Available (Delivery Cost on Buyer) | ||
| OEM | Available | ||
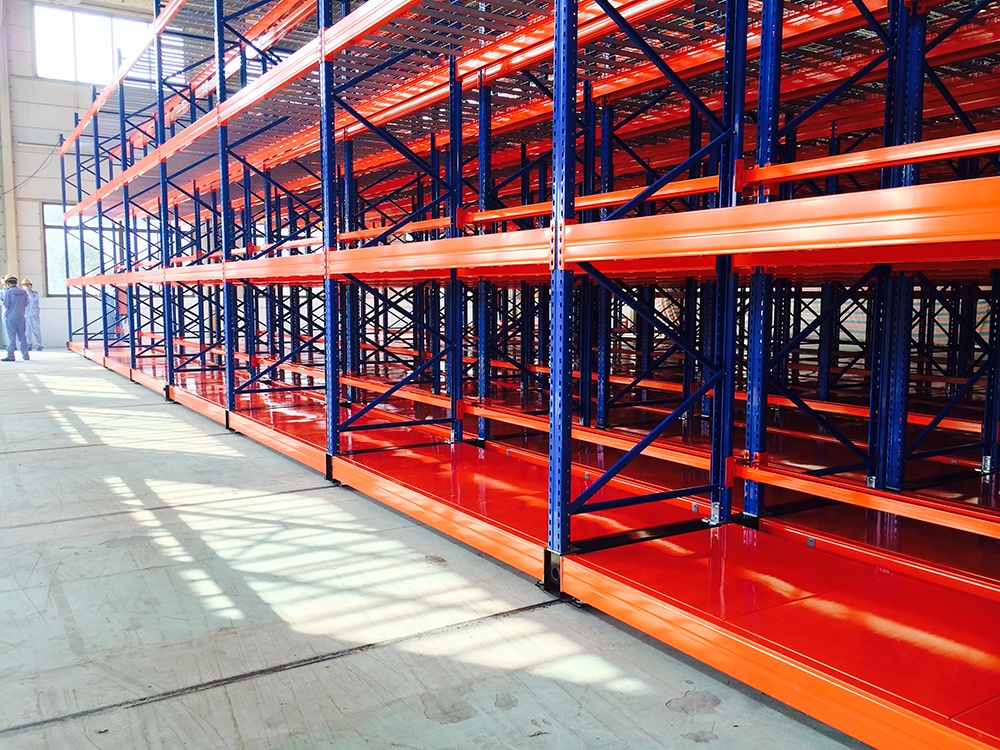
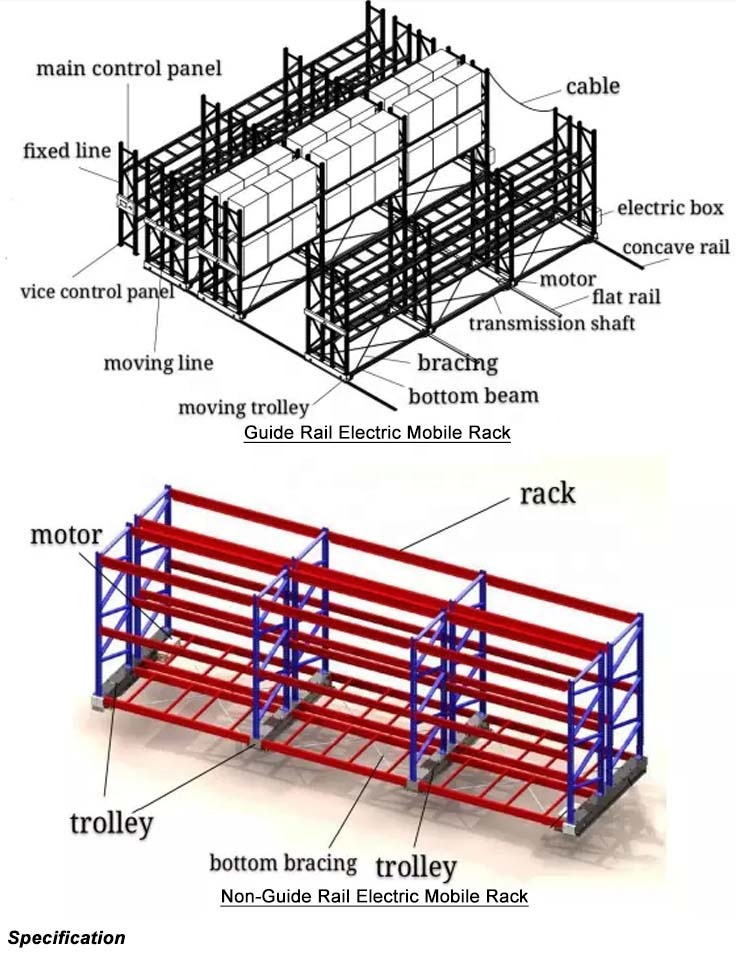
| Technical Parameters | Guide Rail | Non-Guide Rail |
|---|---|---|
| Loading Capacity | 32 tons/unit | 16 tons/unit |
| Wheel Material | Cast Iron | Polyurethane |
| Width of Trolley | 210/226mm | 300mm |
| Cost | Normal | High |
| Running Speed | Max 10m/min | |
| Notch Requirement | Need | No Need |
| Guidance Type | Rail Guidance | Mechanical Guidance |
| Power of Motor | 0.4KW, 0.75KW | |
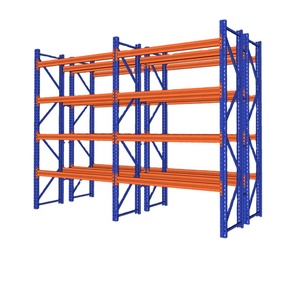
| Rack Part | Pallet Rack |
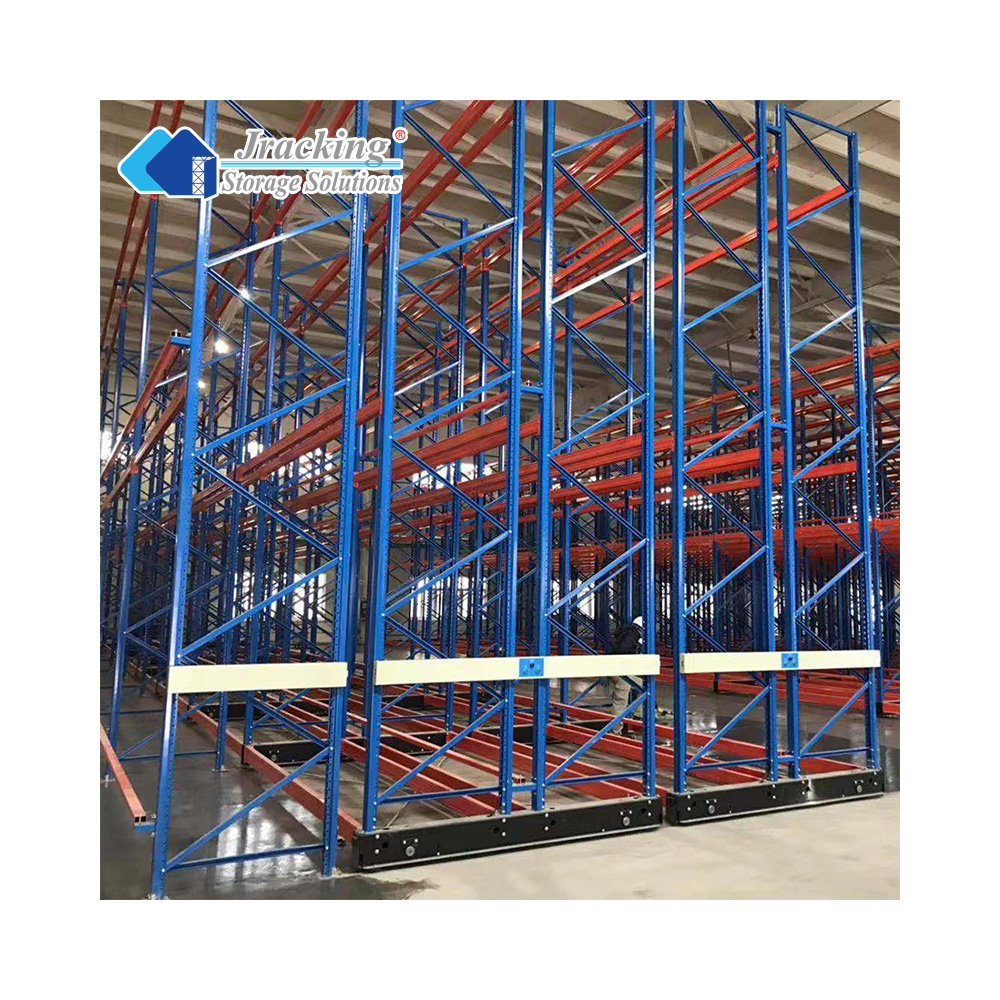
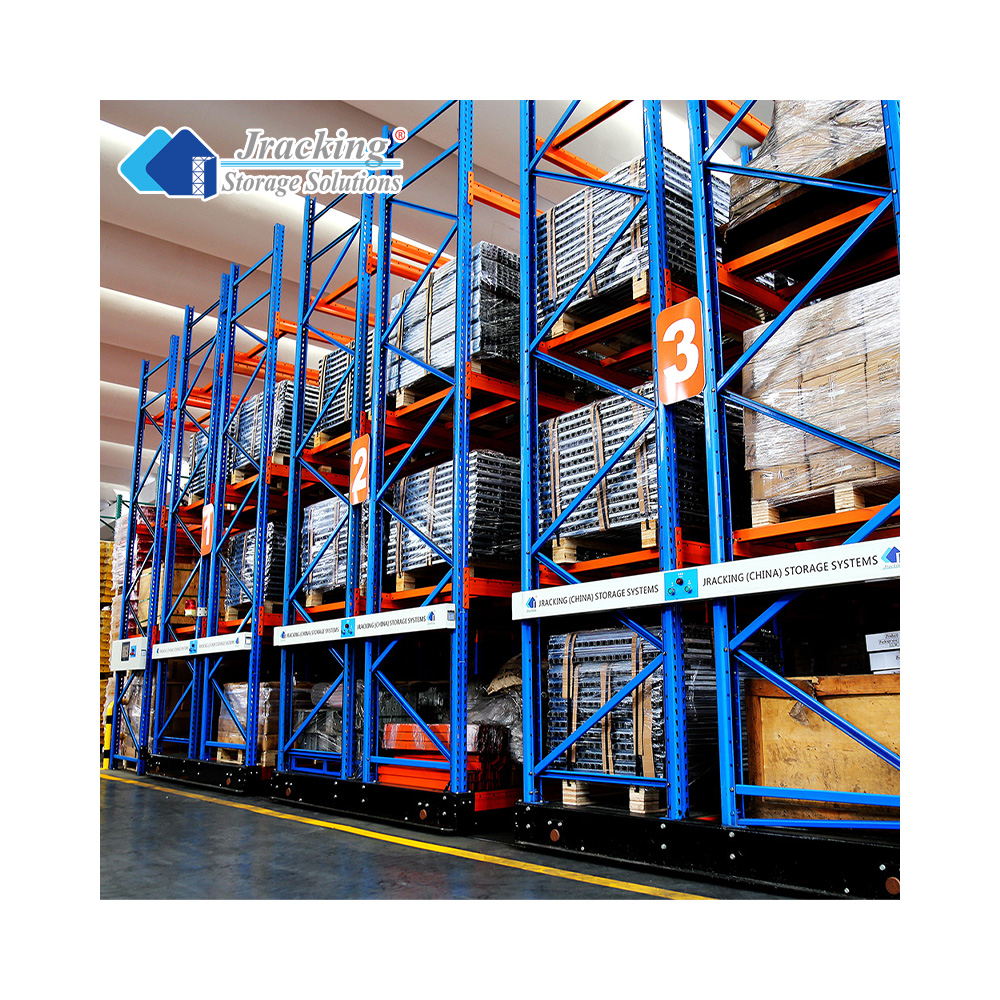
| Transmission Part | Bottom bracing, Trolley, Motor, Transmission shaft |
| Control Part | Control system, Software |
| Guide Part | Guide rail or side guide rail |
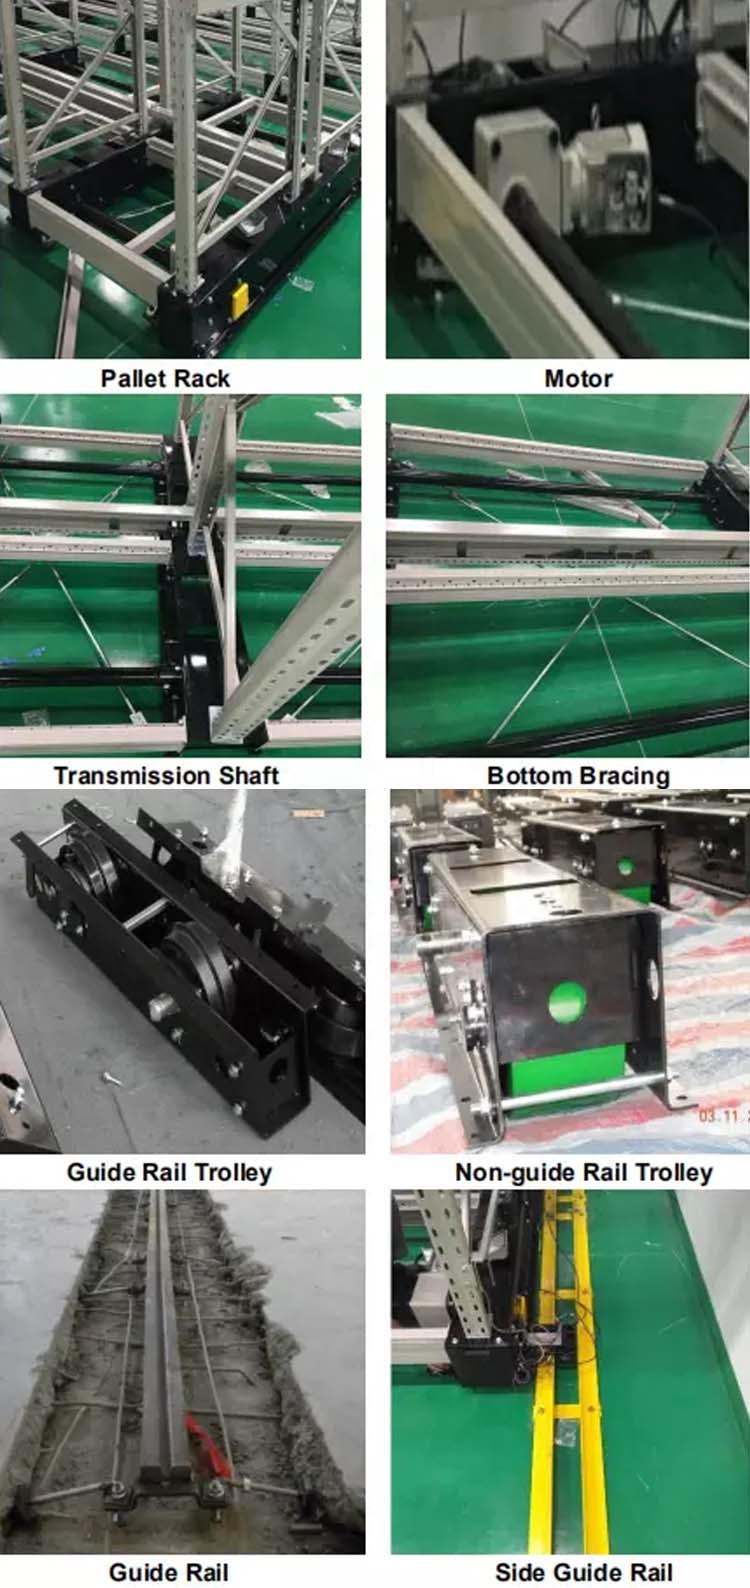
| Guide Rail | Non-Guide Rail |
|---|---|
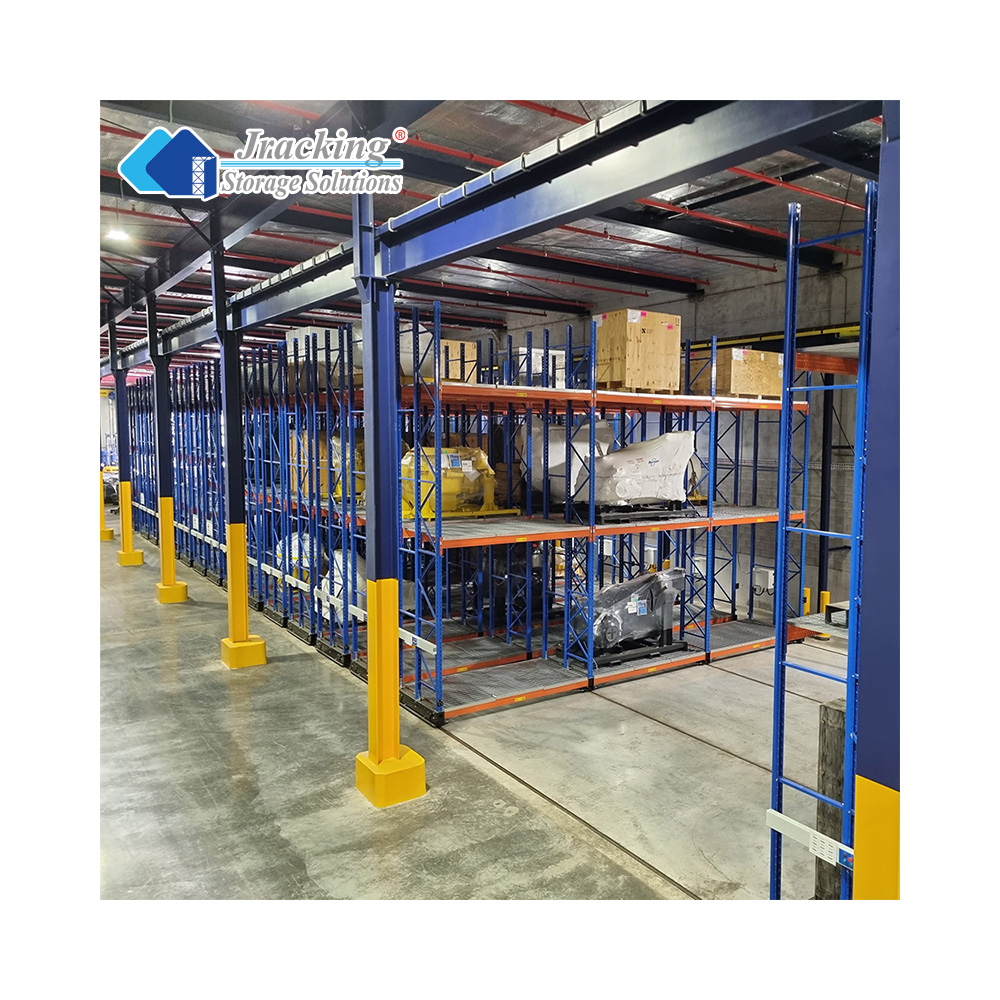
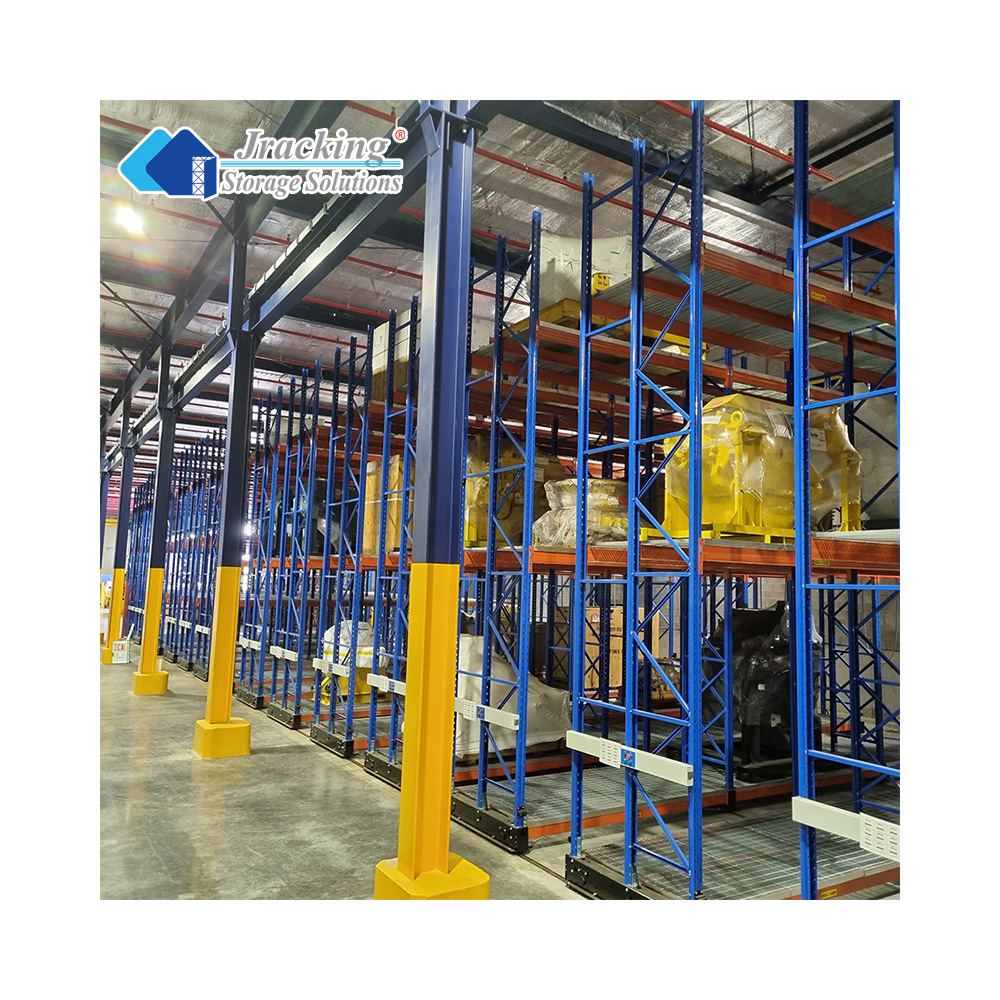
| Guide rail electric mobile rack needs notching, rail laying, pouring and rail maintenance. It is suitable for a warehouse with large load capacity and slotting on the ground. | Non-guide rail electric mobile rack does not need notching. It is suitable for a warehouse with smaller loading requirements and no slotting on the ground. |
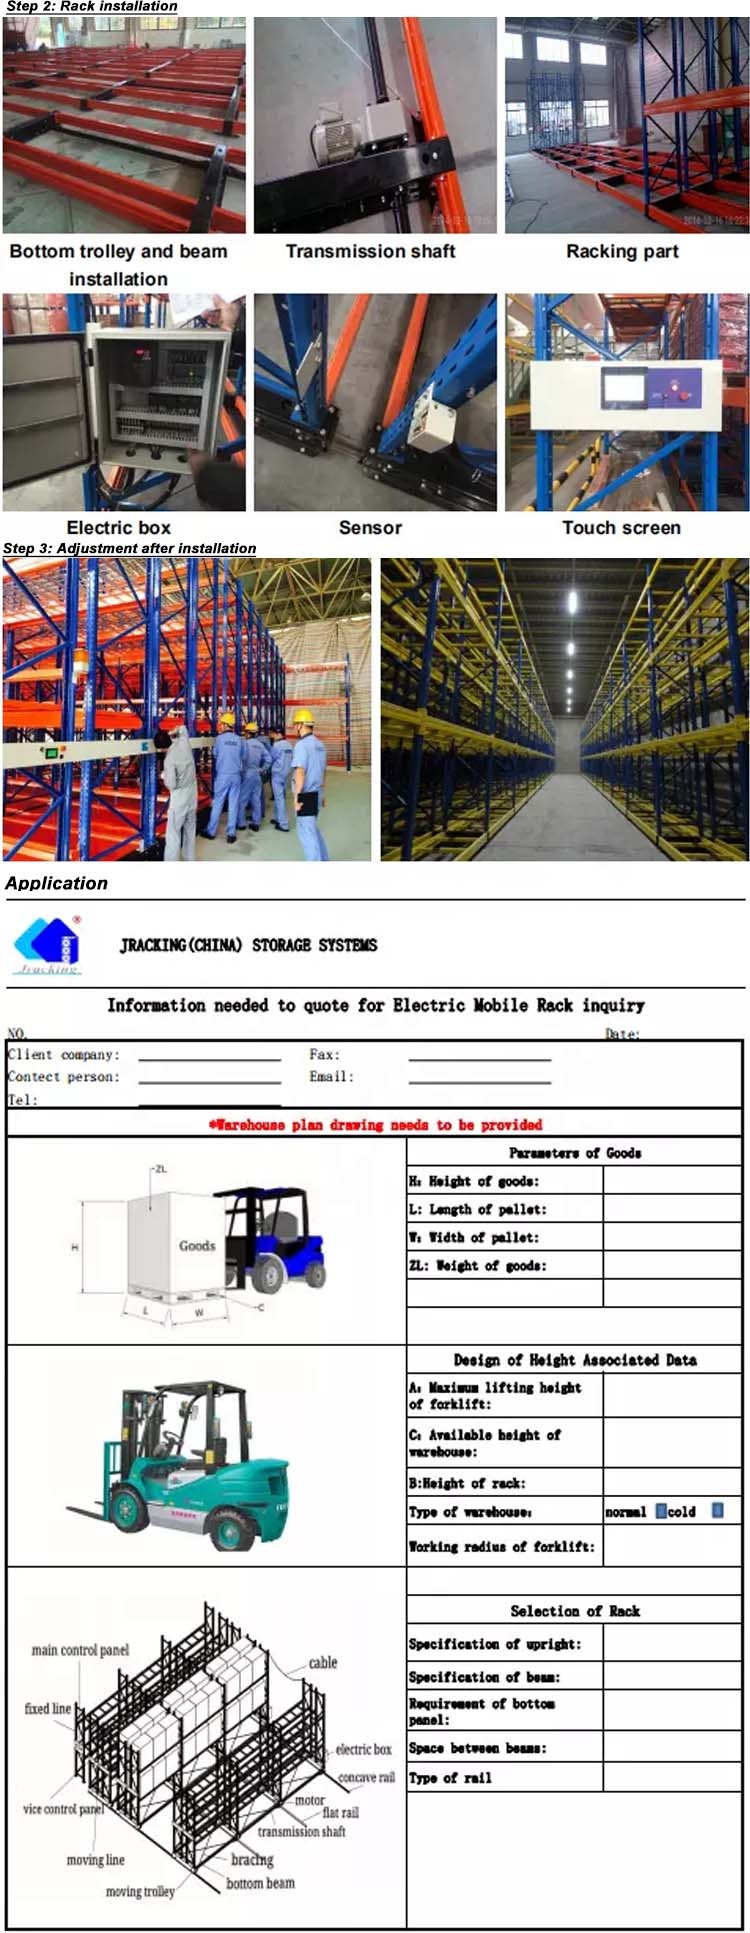
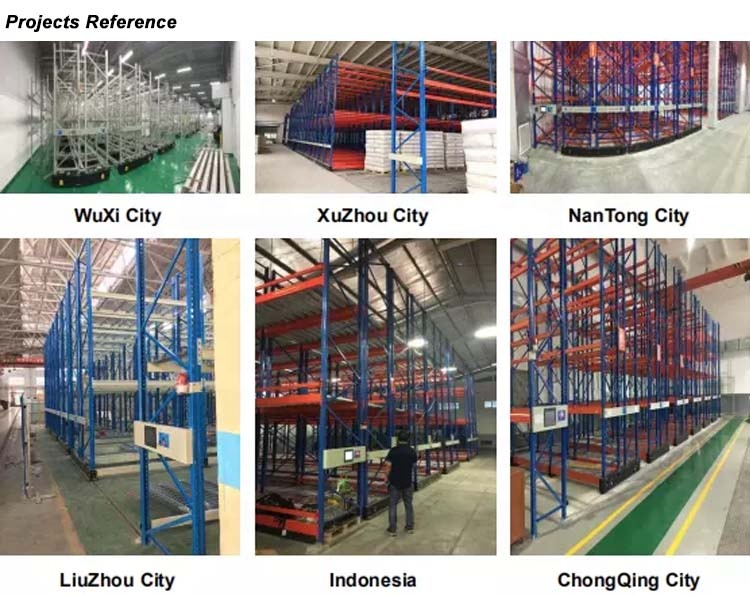
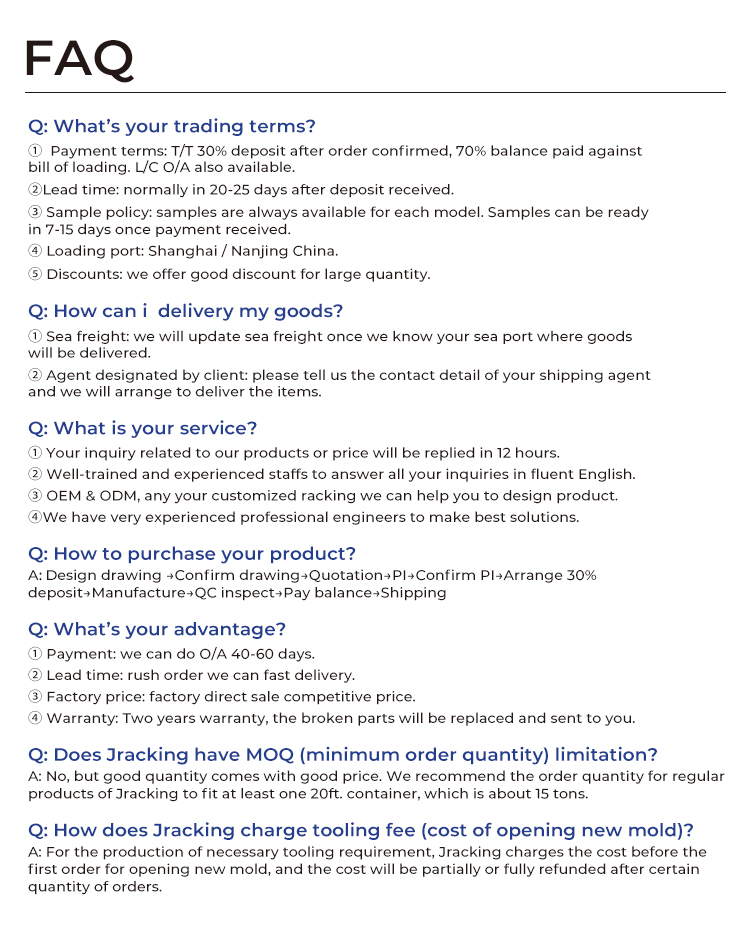
A: Guide rail systems require ground notching and concrete embedment, providing a higher loading capacity up to 32 tons per unit. Non-guide rail units operate via mechanical guidance directly on the existing floor without floor excavation, supporting up to 16 tons per unit.
A: Yes, the system is engineered specifically for optimal performance in cold storage and deep-freeze environments down to low temperatures, offering maximum space utilization to minimize cooling energy expenses.
A: Every mobile racking section is fitted with dedicated detection devices, emergency stop buttons, safety light barriers, and automated transmission interlocks to ensure maximum protection for both operators and inventory.
A: Yes, all structural dimensions, weight capacities, and system configurations are fully customized according to specific warehouse blueprints, pallet sizes, and operational throughput demands.
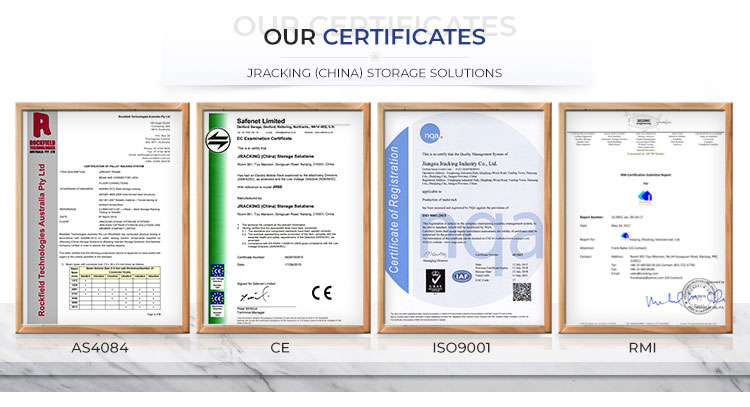
A: The products are certified under international manufacturing standards including CE and ISO9001:2008 certification, guaranteeing rigorous safety, structural integrity, and durability standards.